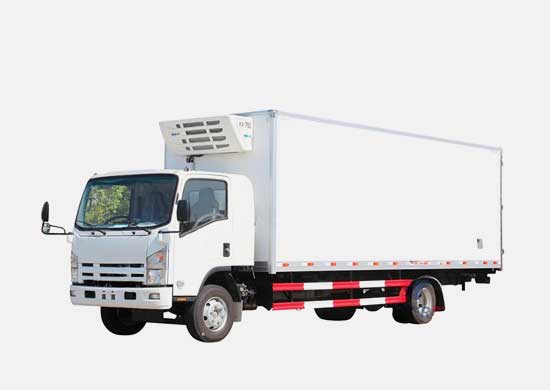
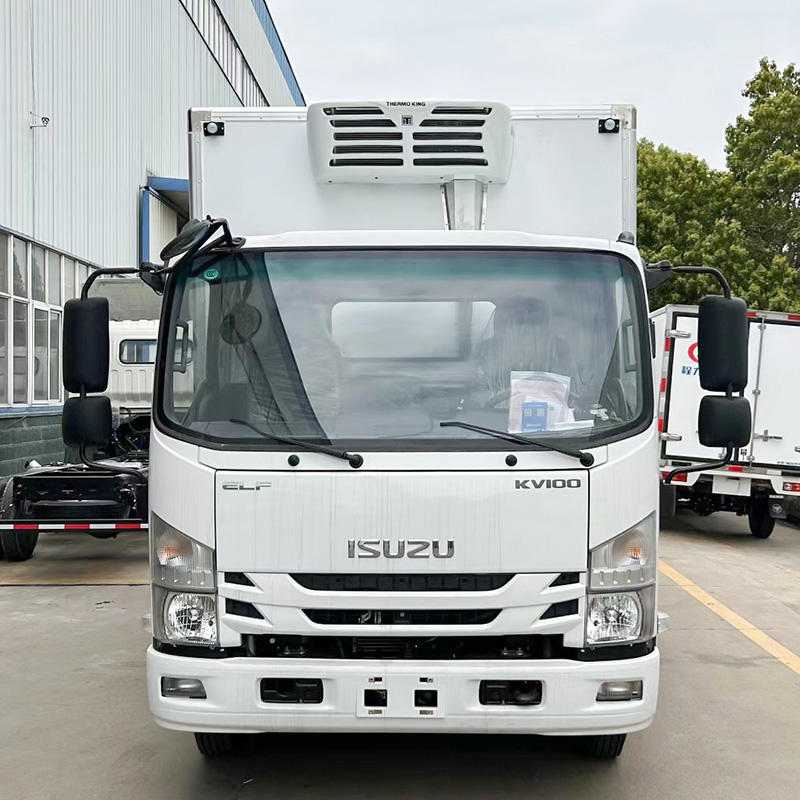
This refrigerated truck is an efficient transportation equipment specially built for cold chain logistics scenarios, with stable and reliable temperature control technology as the core, integrating lightweight design and intelligent management system, which can achieve precise temperature control in a wide range of -25°C~20°C, covering the low-temperature transportation needs of all categories from fresh ingredients to pharmaceutical reagents.
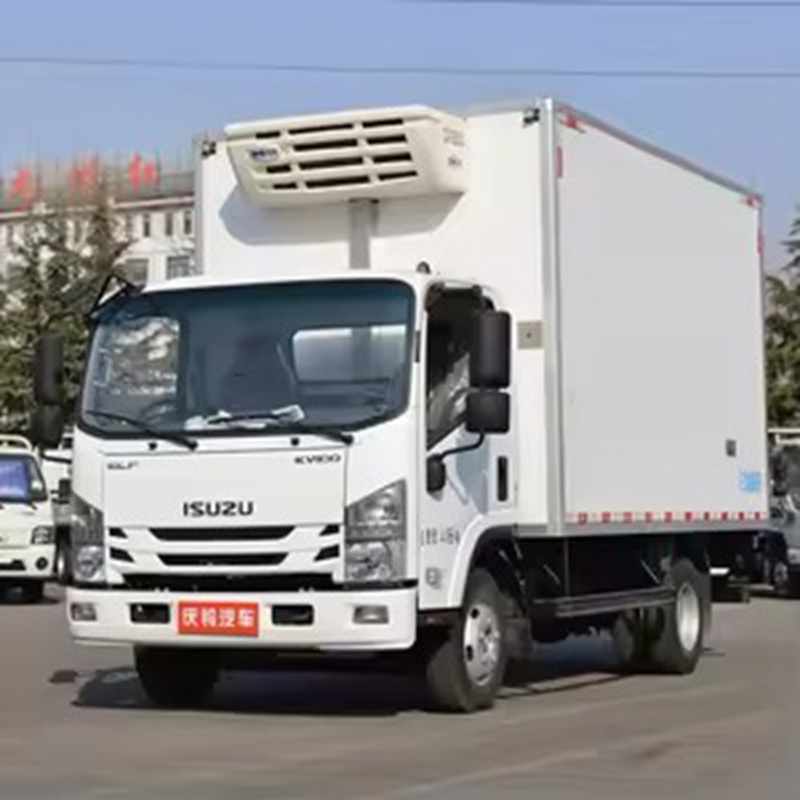
Adopt well-known brand refrigeration units, temperature control accuracy error ≤± 0.5°C, support multi-gear adjustment, meet the exclusive temperature needs of different goods, and use multi-point temperature sensors to monitor temperature changes in the cabin in real time.
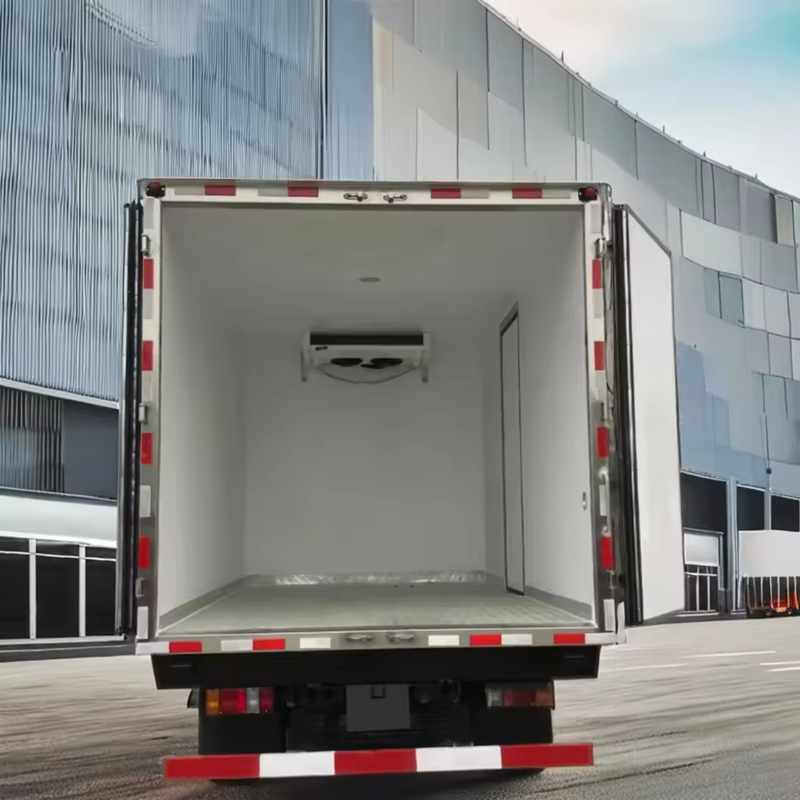
The refrigerated compartment adopts polyurethane high-pressure foaming process, and the inner and outer skins are made of high-quality FRP or stainless steel, with a thickness of 80-120mm, strong airtightness, and can still maintain a low-temperature environment for 4-6 hours when the power is off.
Equipped with on-board intelligent terminals, it supports real-time upload of temperature data, remote monitoring, and abnormal alarm (sound and light + SMS) functions, which can realize the traceability of the whole process of transportation and the retention of temperature records, which meets the requirements of cold chain logistics supervision.
the chassis adopts a mature commercial vehicle platform, stable power output, and the braking system is upgraded and optimized; The compartment is equipped with anti-collision strips, anti-slip floors, and complete cargo fixing devices to ensure the safety of personnel and goods during transportation.
Under the premise of ensuring structural strength, high-strength and lightweight materials are used to build the box body and frame, which effectively reduces the weight of the vehicle and improves loading capacity and fuel economy.
cross-regional transportation of fresh fruits and vegetables, frozen meat, dairy products, seafood and aquatic products, quick-frozen food, etc., to ensure the freshness of ingredients from the place of origin to the table.
constant temperature transportation of vaccines, biological preparations, refrigerated drugs, diagnostic reagents, etc., strictly following the GSP standards of the pharmaceutical cold chain to ensure that the efficacy of drugs is not affected.
Store distribution of supermarket chains and fresh food e-commerce stores supports multi-temperature partition design, which can transport goods with different temperature requirements at the same time to improve distribution efficiency.
Transportation of high-temperature sensitive foods such as ice cream and chocolate, as well as goods that require a specific temperature environment such as flowers and chemical raw materials, to meet personalized low-temperature transportation needs.
If you are interested in purchasing a high-quality refrigerated truck, please contact our sales team today. We provide customized solutions, competitive pricing, and prompt delivery to meet your transportation needs. Reach out via email or phone to discuss your requirements and get a detailed quotation.